| Обновлено 2020-04-15 20:33:41 |
|
Металлорежущий инструмент и инструментальная оснастка для станков / Cutting tools and tooling system KYOCERA | Каталог KYOCERA 2016 Металлорежущий инструмент для точения на станках (Всего 679 стр.) |
|||||
501 Каталог KYOCERA 2016 Металлорежущий инструмент для токарной обработки на станках Стр.H9 |
|||||
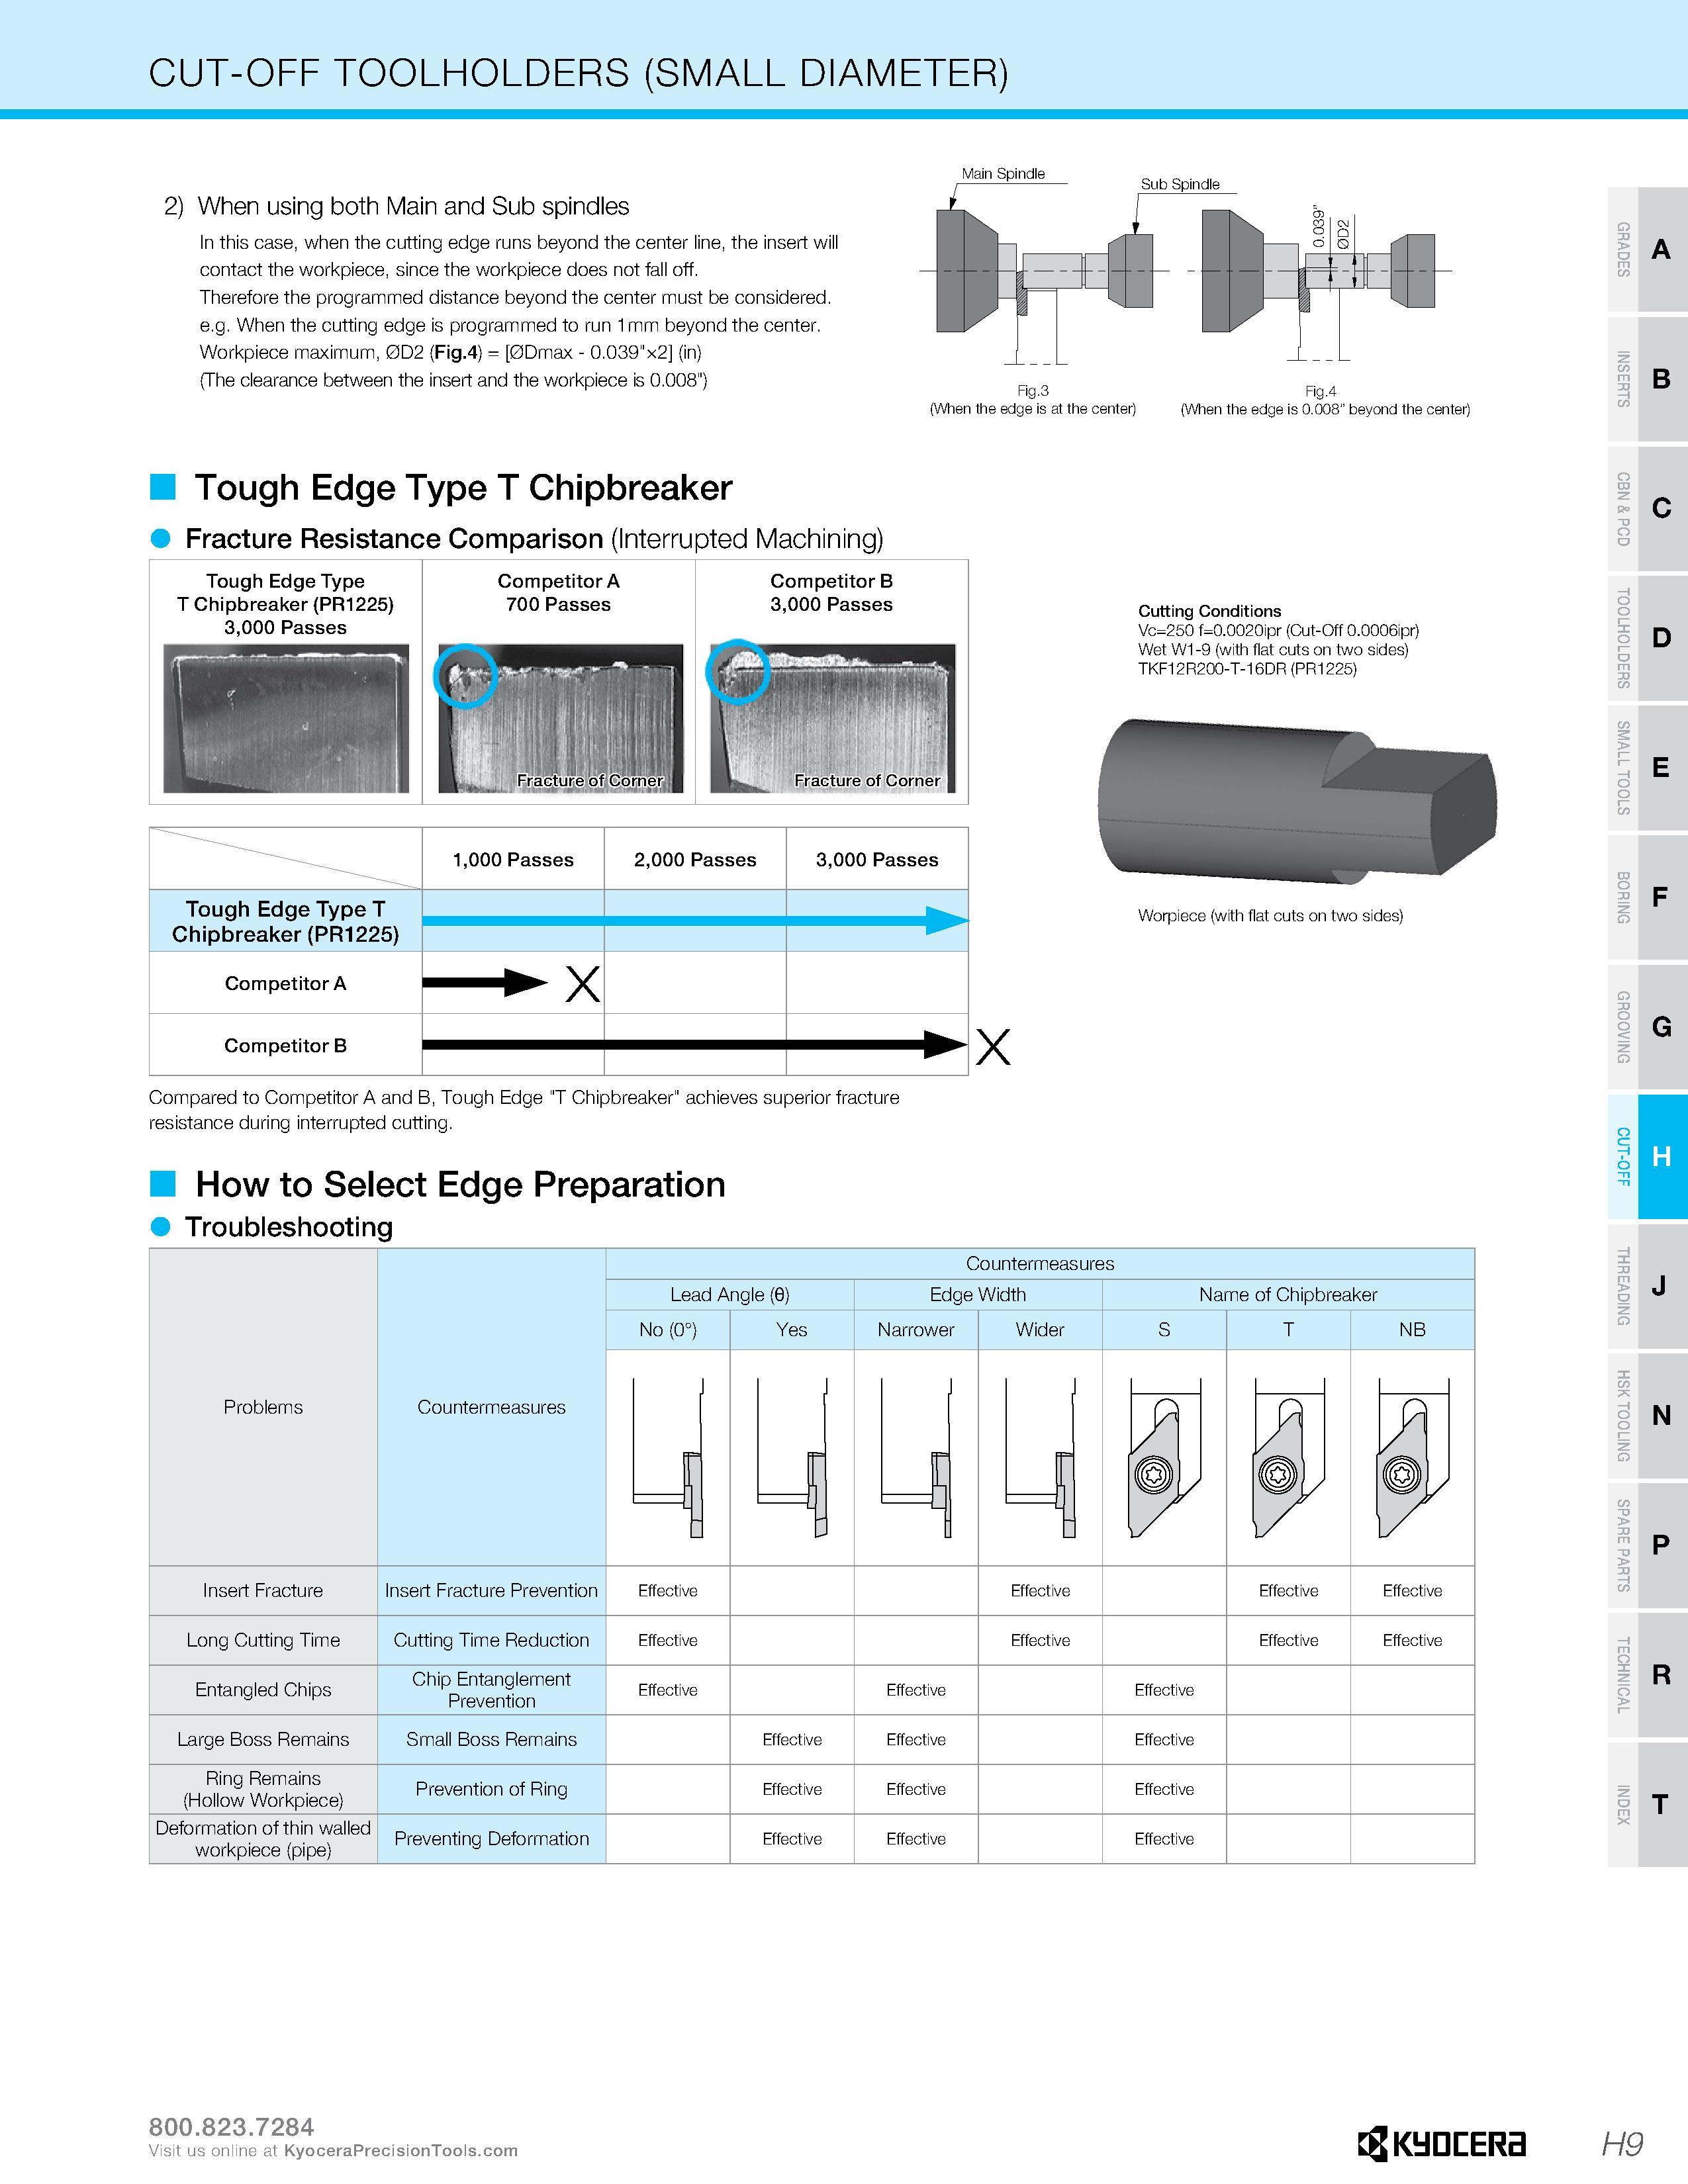
Каталог KYOCERA 2016 Токарные резцы с пластинами Стр. H9 0501 ENG Lab2u CUT-OFF TOOLHOLDERS (SMALL DIAMETER) Main Spindle 2) When using both Main and Sub spindles In this case, when the cutting edge runs beyond the center line, the insert will contact the workpiece, since the workpiece does not fall off. Therefore the programmed distance beyond the center must be considered. e.g. When the cutting edge is programmed to run 1mm beyond the center. Workpiece maximum, 0D2 (Fig.4) = 0Dmax - 0.039"x2 (in) (The clearance between the insert and the workpiece is 0.008") Sub Spindle Fig.3 Fig.4 (When the edge is at the center) (When the edge is 0.008" beyond the center) A B Tough Edge Type T Chipbreaker Fracture Resistance Comparison (Interrupted Machining) Tough Edge Type T Chipbreaker (PR1225) 3,000 Passes Competitor A 700 Passes Competitor B 3,000 Passes Cutting Conditions Vc=250 f=0.0020ipr (Cut-Off 0.0006ipr) Wet W1 -9 (with flat cuts on two sides) TKF12R200-T-16DR (PR1225) 1,000 Passes 2,000 Passes 3,000 Passes Tough Edge Type T Chipbreaker (PR1225) Competitor A X Competitor B Worpiece (with flat cuts on two sides) X Compared to Competitor A and B, Tough Edge "T Chipbreaker" achieves superior fracture resistance during interrupted cutting. How to Select Edge Preparation Troubleshooting Problems Insert Fracture Long Cutting Time Entangled Chips Large Boss Remains Ring Remains (Hollow Workpiece) Deformation of thin walled workpiece (pipe) Countermeasures Lead Angle ( No (0°) Countermeasures Insert Fracture Prevention Cutting Time Reduction Chip Entanglement Prevention Small Boss Remains Prevention of Ring Preventing Deformation Yes Edge Width Narrower Wider Name of Chipbreaker T NB C D E G N P R T F J S Effective Effective Effective Effective Effective Effective Effective Effective Effective Effective Effective Effective Effective Effective Effective Effective Effective Effective Effective Effective Kyocera H9 |
|||||
См.также / See also : |
|||||
Соотношение твердостей Таблица / Hardness equivalent table |
Аналоги марок стали / Workpiece material conversion table |
||||
Отклонение размера детали / Fit tolerance table |
Перевод оборотов в скорость / Surface speed to RPM conversion |
||||
Диаметр под резьбу / Tap drill sizes |
Виды резьбы в машиностроении / Thread types and applications |
||||
Дюймы в мм Таблица / Inches to mm Conversion table |
Современные инструментальные материалы / Cutting tool materials |
||||
| |
|||||
| KYOCERA | |||||
| |
|||||
 Каталог KYOCERA 2017 Инструмент режущий для металлорежущих станков (англ.яз / ENG) (1072 страницы) |
|||||
 Каталог KYOCERA 2016 Режущий инструмент для станков (англ.яз / ENG) (992 страницы) |
 Каталог KYOCERA 2016 Металлорежущий инструмент для точения на станках (англ.яз / ENG) (679 страниц) |
 Каталог KYOCERA 2016 Фрезерный металлорежущий инструмент с СРП (англ.яз / ENG) (335 страниц) |
 Каталог KYOCERA 2016 Твердосплавный вращающийся режущий инструмент (англ.яз / ENG) (315 страниц) |
 Каталог KYOCERA 2015 Инструмент режущий для мелкоразмерной обработки (англ.яз / ENG) (406 страниц) |
 Каталог KYOCERA 2014 Металлорежущий инструмент (англ.яз / ENG) (885 страниц) |
 Каталог KYOCERA 2011 Металлорежущий инструмент (англ.яз / ENG) (835 страниц) |
|||||
| |
|||||
|
Каталоги инструмента и оснастки для металлообработки на станках / Cutting tools and tooling system catalogs |
|||||
| Каталог KYOCERA 2016 Металлорежущий инструмент для точения на станках (Всего 679 стр.) | |||||
| |
|||||
 498 |  499 |  500 |  502 |  503 |  504 |
|
Lab2U | Catalogs | Tap drill sizes | Speed to RPM | Material table Разработчики сайта / Developers of site |
|
Поиск на сайте Lab2u.ru с помощью поисковых систем ЯНДЕКС, BING, GOOGLE:
|
||
|
|
||
