| Обновлено 2020-04-16 13:10:01 |
|
Режущий инструмент, инструментальная оснастка и приспособления / Cutting tools, tooling system and workholding
WALTER | Каталог WALTER 2012 Инструмент и оснастка Valenite (Всего 2590 стр.) |
|||||
|
1080 Каталог WALTER 2012 Металлорежущий инструмент и инструментальная оснастка Valenite Стр.C178 |
|||||
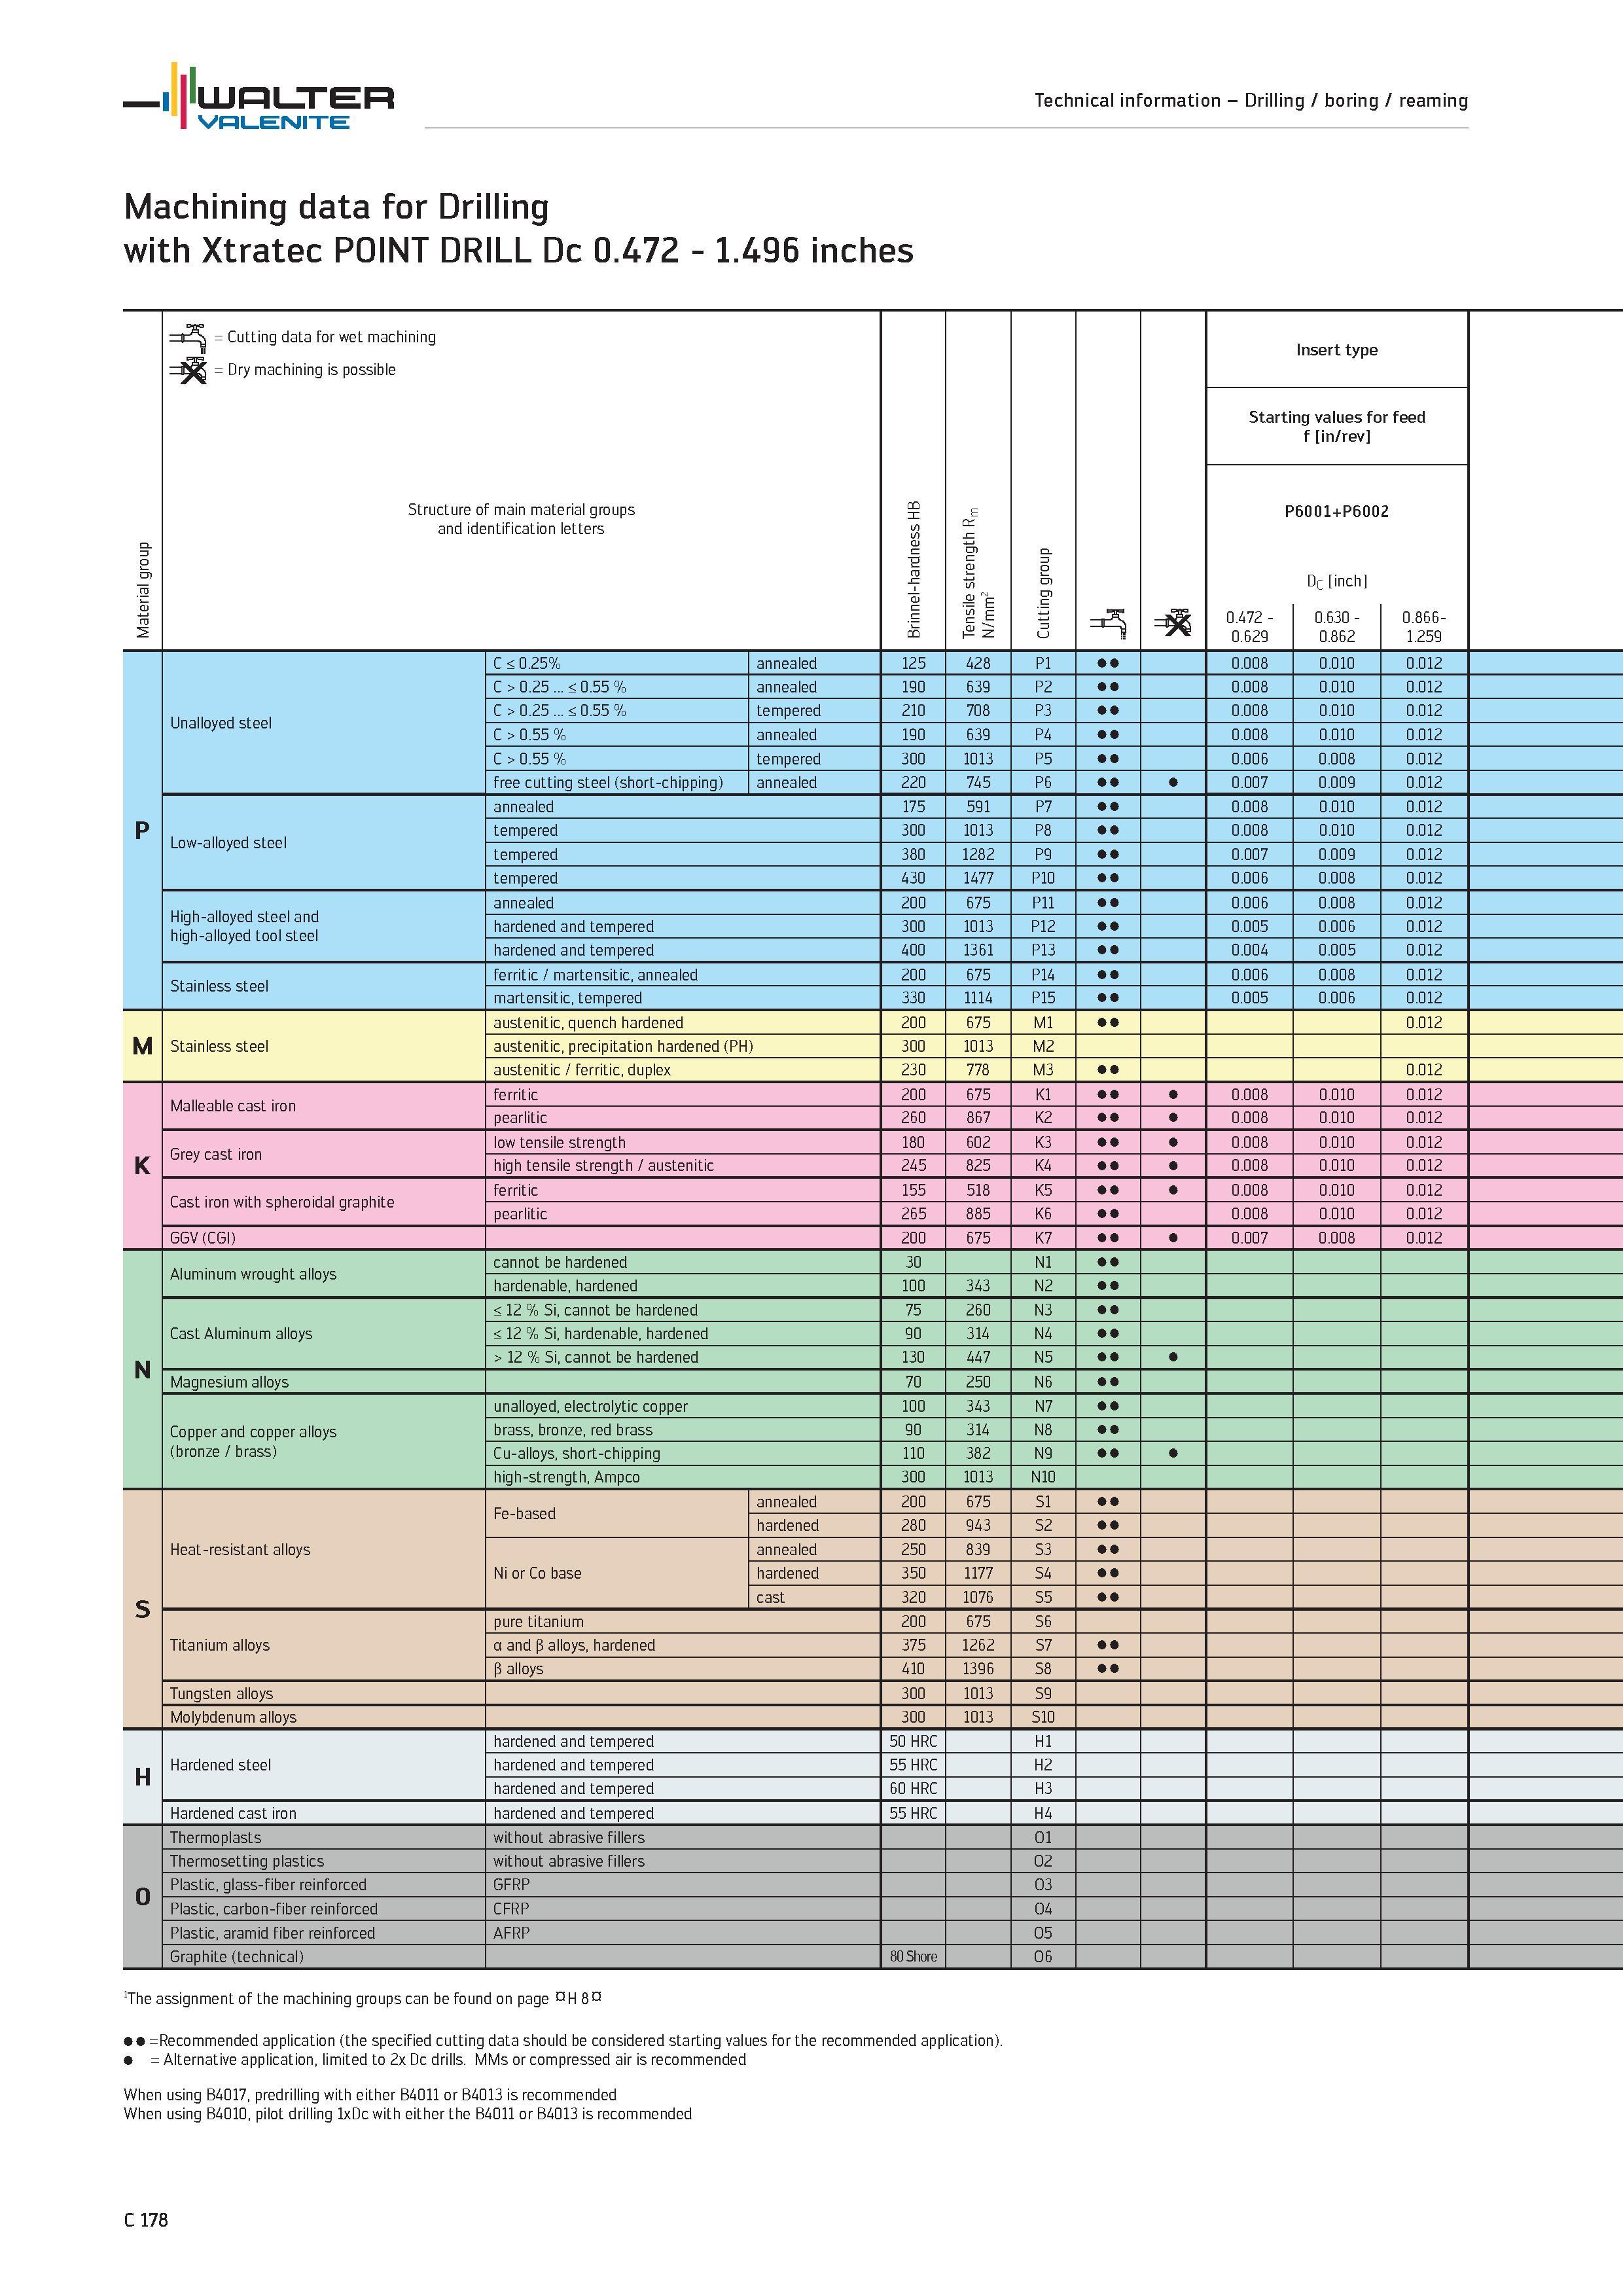
Machining data for Drilling with Xtratec POINT DRILL WALTER Dc 0 472 1 496 inches Material group Cutting data for wet machining Dry machining isMachining data for Drilling with Xtratec POINT DRILL WALTER Dc 0.472 1.496 inches Material group Cutting data for wet machining Dry machining is possible Structure of main material groups and identification letters Brinnel-hardness HB Tensile strength Rm N/mm2 Cutting group 3 Starti P 0.472 -0.629 Insert type ng values fo f in/rev 6001+P600 Dc inch 0.630 -0.862 r feed 2 0.866- 1.259 p Unalloyed steel C < 0.25% annealed 125 428 P1 0.008 0.010 0.012 C > 0.25 < 0.55 % annealed 190 639 P2 0.008 0.010 0.012 C > 0.25 < 0.55 % tempered 210 708 P3 0.008 0.010 0.012 C > 0.55 % annealed 190 639 P4 0.008 0.010 0.012 C > 0.55 % tempered 300 1013 P5 0.006 0.008 0.012 free cutting steel (short-chipping) annealed 220 745 P6 0.007 0.009 0.012 Low-alloyed steel annealed 175 591 P7 0.008 0.010 0.012 tempered 300 1013 P8 0.008 0.010 0.012 tempered 380 1282 P9 0.007 0.009 0.012 tempered 430 1477 P10 0.006 0.008 0.012 High-alloyed steel and high-alloyed tool steel annealed 200 675 P11 0.006 0.008 0.012 hardened and tempered 300 1013 P12 0.005 0.006 0.012 hardened and tempered 400 1361 P13 0.004 0.005 0.012 Stainless steel ferritic / martensitic, annealed 200 675 P14 0.006 0.008 0.012 martensitic, tempered 330 1114 P15 0.005 0.006 0.012 M Stainless steel austenitic, quench hardened 200 675 M1 0.012 austenitic, precipitation hardened (PH) 300 1013 M2 austenitic / ferritic, duplex 230 778 M3 0.012 K Malleable cast iron ferritic 200 675 K1 0.008 0.010 0.012 pearlitic 260 867 K2 0.008 0.010 0.012 Grey cast iron low tensile strength 180 602 K3 0.008 0.010 0.012 high tensile strength / austenitic 245 825 K4 0.008 0.010 0.012 Cast iron with spheroidal graphite ferritic 155 518 K5 0.008 0.010 0.012 pearlitic 265 885 K6 0.008 0.010 0.012 GGV (CGI) 200 675 K7 0.007 0.008 0.012 N Aluminum wrought alloys cannot be hardened 30 N1 hardenable, hardened 100 343 N2 Cast Aluminum alloys < 12 % Si, cannot be hardened 75 260 N3 < 12 % Si, hardenable, hardened 90 314 N4 > 12 % Si, cannot be hardened 130 447 N5 Magnesium alloys 70 250 N6 Copper and copper alloys (bronze / brass) unalloyed, electrolytic copper 100 343 N7 brass, bronze, red brass 90 314 N8 Cu-alloys, short-chipping 110 382 N9 high-strength, Ampco 300 1013 N10 S Heat-resistant alloys Fe-based annealed 200 675 S1 hardened 280 943 S2 Ni or Co base annealed 250 839 S3 hardened 350 1177 S4 cast 320 1076 S5 Titanium alloys pure titanium 200 675 S6 a and p alloys, hardened 375 1262 S7 P alloys 410 1396 S8 Tungsten alloys 300 1013 S9 Molybdenum alloys 300 1013 S10 H Hardened steel hardened and tempered 50 HRC H1 hardened and tempered 55 HRC H2 hardened and tempered 60 HRC H3 Hardened cast iron hardened and tempered 55 HRC H4 O Thermoplasts without abrasive fillers O1 Thermosetting plastics without abrasive fillers O2 Plastic, glass-fiber reinforced GFRP O3 Plastic, carbon-fiber reinforced CFRP O4 Plastic, aramid fiber reinforced AFRP O5 Graphite (technical) 80 Shore O6 1The assignment of the machining groups can be found on page °H 8° =Recommended application (the specified cutting data should be considered starting values for the recommended application). Alternative application, limited to 2x Dc drills. MMs or compressed air is recommended When using B4017, predrilling with either B4011 or B4013 is recommended When using B4010, pilot drilling 1xDc with either the B4011 or B4013 is recommended C 178 WALTER Valenite Technical information Drilling / boring / reaming |
|||||
См.также / See also : |
|||||
Расчет режимов резания при токарной обработке / Turning formulas |
Расчет режимов резания при сверлении / Formulas for drilling |
||||
Аналоги сталей Таблицы / Workpiece material conversion table |
Расчет режимов резания при фрезеровании / Milling formulas |
||||
Группы конструкционных материалов / Workpiece material groups |
Удельная сила резания / Specific cutting force |
||||
Техника безопасности при работе с инструментом / Metal cutting safety |
Производительность режущего инструмента / Machining economy |
||||
| |
|||||
| WALTER | |||||
| |
 Каталог WALTER 2017 Инструмент и оснастка для станков (2605 страниц) |
 Каталог WALTER 2016 Общий Инструмент режущий и оснастка (нем.яз. / DEU) (2605 страниц) |
 Каталог WALTER 2016 Новый инструмент для металлообработки Вер. 16-2 (276 страниц) |
 Каталог WALTER 2016 Продукция для металлообработки Инновации Вер. 16-1 (116 страниц) |
 Каталог WALTER 2015 Новый инструмент и оснастка 2015-1 (336 страниц) |
 Каталог WALTER 2014 Новая продукция 14-2 (324 страницы) |
 Каталог WALTER 2013 Новая инструментальная продукция Инновации Вер 13-1 (276 страниц) |
 Каталог WALTER 2013 Дополнение к общему (832 страниц) |
 Каталог WALTER 2012 Новинки Инструмент для мехобработки Вер 12-2 (232 страницы) |
 Каталог WALTER 2012 Инструмент и оснастка (2148 страниц) |
 Каталог WALTER 2012 Инструмент и оснастка Valenite (англ.яз / ENG) (2590 страниц) |
 Каталог WALTER 2008 Новый металлорежущий инструмент (215 страниц) |
 Каталог WALTER 2007 Режущий инструмент и оснастка (830 страниц) |
|||||
| |
|||||
|
Каталоги инструмента и оснастки для металлообработки на станках / Cutting tools and tooling system catalogs |
|||||
| Каталог WALTER 2012 Инструмент и оснастка Valenite (Всего 2590 стр.) | |||||
| |
|||||
 1077 |  1078 |  1079 |  1081 | 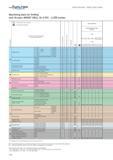 1082 |  1083 |
|
Lab2U | Catalogs | Tap drill sizes | Speed to RPM | Material table Разработчики сайта / Developers of site |
|
Поиск на сайте Lab2u.ru с помощью поисковых систем ЯНДЕКС, BING, GOOGLE:
|
||
|
|
||
