| Обновлено 2020-04-18 13:44:59 |
|
Металлорежущий инструмент и инструментальная оснастка / Cutting tools and tooling system SUMITOMO | Каталог SUMITOMO 2015 Режущий инструмент и оснастка (Всего 602 стр.) |
|||||
Осевой режущий твердосплавный инструмент Sumitomo для сверления глубоких отверстий в металле Спиральные монолитные сверла Сумитомо из твердого сплава Рек454 Каталог SUMITOMO 2015 Режущий инструмент и инструментальная оснастка Стр.450 |
|||||
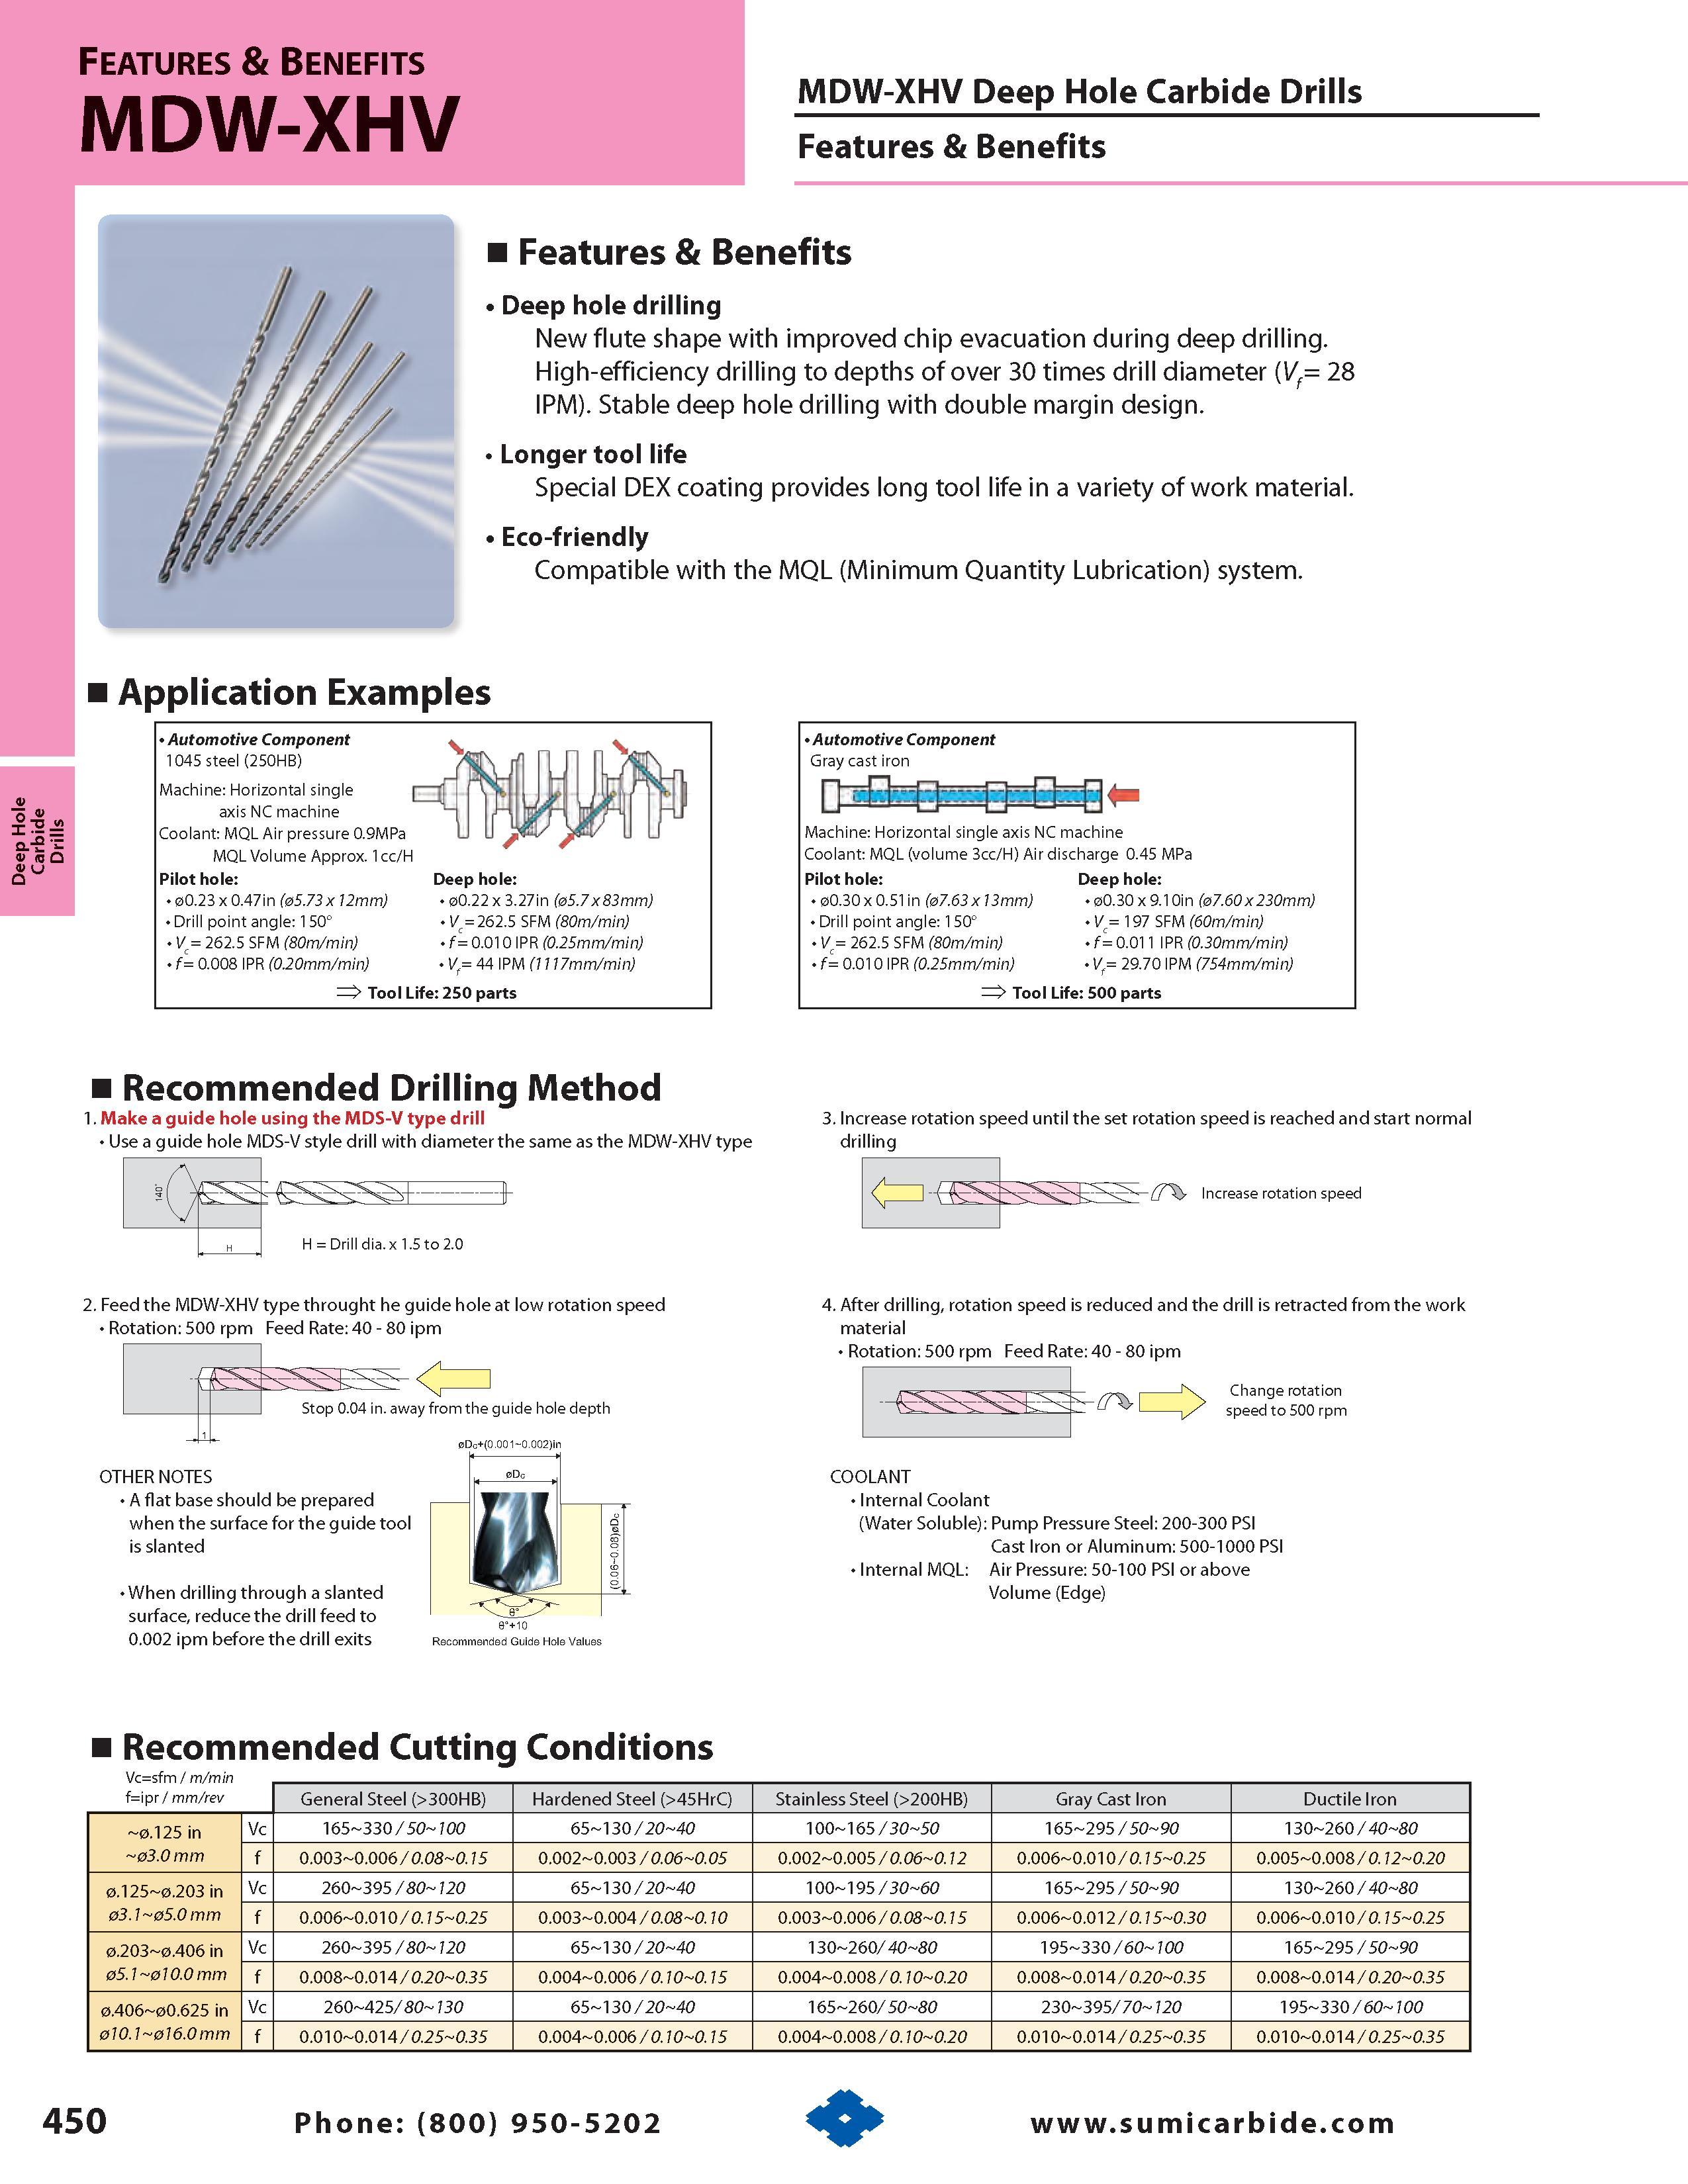
Осевой режущий твердосплавный инструмент Sumitomo для сверления глубоких отверстий в металле Спиральные монолитные сверла Сумитомо из твердого сплава Рек Осевой режущий твердосплавный инструмент Sumitomo для сверления глубоких отверстий в металле Спиральные монолитные сверла Сумитомо из твердого сплава Рекомендации японского производителя по технологии обработки и режимам резания Deep Hole Carbide Drills Features & Benefits MDW-XHV MDW-XHV Deep Hole Carbide Drills Features & Benefits Features & Benefits Deep hole drilling New flute shape with improved chip evacuation during deep drilling High-efficiency drilling to depths of over 30 times drill diameter (Vf= 28 IPM). Stable deep hole drilling with double margin design. Longer tool life Special DEX coating provides long tool life in a variety of work material. Eco-friendly Compatible with the MQL (Minimum Quantity Lubrication) system Application Examples Automotive Component 1045 steel (250HB) Machine Horizontal single axis NC machine Coolant MQL Air pressure 0.9MPa MQL Volume Approx. 1 cc/H Pilot hole 00.23 x 0.47in (05.73 x 12mm) Drill point angle 150° V = 262. 5 SFM (80m/min) f = 0.008 IPR (0.20mm/min) Tool Life 250 parts Deep hole 00.22 x 3.27in (05.7 x 83mm) V = 262.5 SFM (80m/min) f = 0 010 IPR (0.25mm/min) V = 44 ipm (1117mm/min) Automotive Component Gray cast iron Machine Horizontal single axis NC machine Coolant MQL (volume 3cc/H) Air discharge 0. 45 MPa Pilot hole 00.30 x 0.51in (07.63 x 13mm) Drill point angle 150° Vc = 262.5 SFM (80m/min) f = 0 010 IPR (0.25mm/min) Deep hole 00.30 x 9.10in (07.60 x 230mm) Vc = 197 SFM (60m/min) f = 0. 011 IPR (0.30mm/min) Vf = 29.70 IPM (754mm/min) Tool Life 500 parts Recommended Drilling Method 1. Make a guide hole using the MDS-V type drill Use a guide hole MDS-V style drill with diameter the same as the MDW-XHV type H = Drill dia. x 1.5 to 2.0 3 Increase rotation speed until the set rotation speed is reached and start normal drilling / 1 / /PS Increase rotation speed 2 Feed the MDW-XHV type throught he guide hole at low rotation speed Rotation 500 rpm Feed Rate 40 - 80 ipm Stop 0 04 in. away from the guide hole depth 0Dc+(O.OO1 O.OO2)in OTHER NOTES A flat base should be prepared when the surface for the guide tool is slanted When drilling through a slanted surface, reduce the drill feed to 0 002 ipm before the drill exits 4 After drilling, rotation speed is reduced and the drill is retracted from the work material Rotation 500 rpm Feed Rate 40 - 80 ipm -tr Change rotation speed to 500 rpm COOLANT Internal Coolant (Water Soluble) Pump Pressure Steel 200-300 PSI Cast Iron or Aluminum 500-1000 PSI Internal MQL Air Pressure 50-100 PSI or above Volume (Edge) Recommended Guide Hole Values Recommended Cutting Conditions Vc=sfm / m/min f=ipr / mm/rev General Steel (>300HB) Hardened Steel (>45HrC) Stainless Steel (>200HB) Gray Cast Iron Ductile Iron -0.125 in -03.0 mm Vc 165-330 / 50-100 65-130/20-40 100-165/30-50 165-295 / 50-90 130-260/40-80 f 0.003-0.006/0.08-0.15 0.002-0.003 / 0.06-0.05 0.002-0.005 / 0.06-0.12 0.006-0.010/0.15-0.25 0.005-0.008/0.12-0.20 0.125-0.203 in 03.1-05.0 mm Vc 260-395 /80-120 65 130/20-40 100-195/30-60 165-295 / 50-90 130-260/40-80 f 0.006-0.010/0.15-0.25 0.003-0.004 /0.08-0.10 0.003-0.006/0.08-0.15 0.006-0.012 / 0.15-0.30 0.006-0.010/0.15-0.25 0.203-0.406 in 05.1-010.0 mm Vc 260-395 /80-120 65-130/20-40 130-260/40-80 195-330 /60-100 165-295/50-90 f 0.008-0.014/0.20-0.35 0.004-0.006 /0.10-0.15 0.004-0.008/0.10-0.20 0.008-0.014/0.20-0.35 0.008-0.014/0.20-0.35 0.406-00.625 in 010.1-016.0 mm Vc 260-425/80-130 65-130/20-40 165-260/50-80 230-395/70-120 195-330 / 60-100 f 0 .010-0 .014 / 0.25-0.35 0.004-0.006 /0.10-0.15 0.004-0.008/0.10-0.20 0 .010-0 .014 / 0.25-0.35 0 .010-0 .014 / 0.25-0.35 450 |
|||||
См.также / See also : |
|||||
Оснастка для токарных станков по металлу / Lathe tool holders |
Оснастка для сверлильных и фрезерных станков / Tool holders for drilling and milling |
||||
Термопатроны / Shrink fit chuck |
Гидравлический патрон инструментальный / Hydraulic chucks |
||||
Хвостовики инструментов / Shank tool |
Резьбонарезные патроны для метчиков / Tapping chucks |
||||
Балансировка инструмента / Tool balancing |
Штревель / Pull stud |
||||
| |
|||||
| SUMITOMO | |||||
| |
|||||
 Каталог SUMITOMO 2018 Инструмент металлорежущий англ.яз / ENG) (608 страниц) |
|||||
 Каталог SUMITOMO 2016 Инструмент металлорежущий для станков (976 страниц) |
|||||
 Каталог SUMITOMO 2015 Режущий инструмент и оснастка (англ.яз / ENG) (602 страницы) |
 Каталог SUMITOMO 2014 Сборный и монолитный металлорежущий инструмент (534 страницы) |
 Каталог SUMITOMO 2011 Металлорежущий инструмент (397 страниц) |
|||
| |
|||||
|
Каталоги инструмента и оснастки для металлообработки на станках / Cutting tools and tooling system catalogs |
|||||
| Каталог SUMITOMO 2015 Режущий инструмент и оснастка (Всего 602 стр.) | |||||
| |
|||||
 451 |  452 |  453 |  455 |  456 Метрические твердосплавные цельные сверла Sumitomo MDW-XHV для высокопроизводительного сверления отверстий в металле и сплавах глубиной до 12 диаметров о |  457 |
|
Lab2U | Catalogs | Tap drill sizes | Speed to RPM | Material table Разработчики сайта / Developers of site |
|
Поиск на сайте Lab2u.ru с помощью поисковых систем ЯНДЕКС, BING, GOOGLE:
|
||
|
|
||
