| Обновлено 2020-04-15 20:33:40 |
|
Металлорежущий инструмент и инструментальная оснастка для станков / Cutting tools and tooling system KYOCERA | Каталог KYOCERA 2016 Металлорежущий инструмент для точения на станках (Всего 679 стр.) |
|||||
150 Каталог KYOCERA 2016 Металлорежущий инструмент для токарной обработки на станках Стр.C22 |
|||||
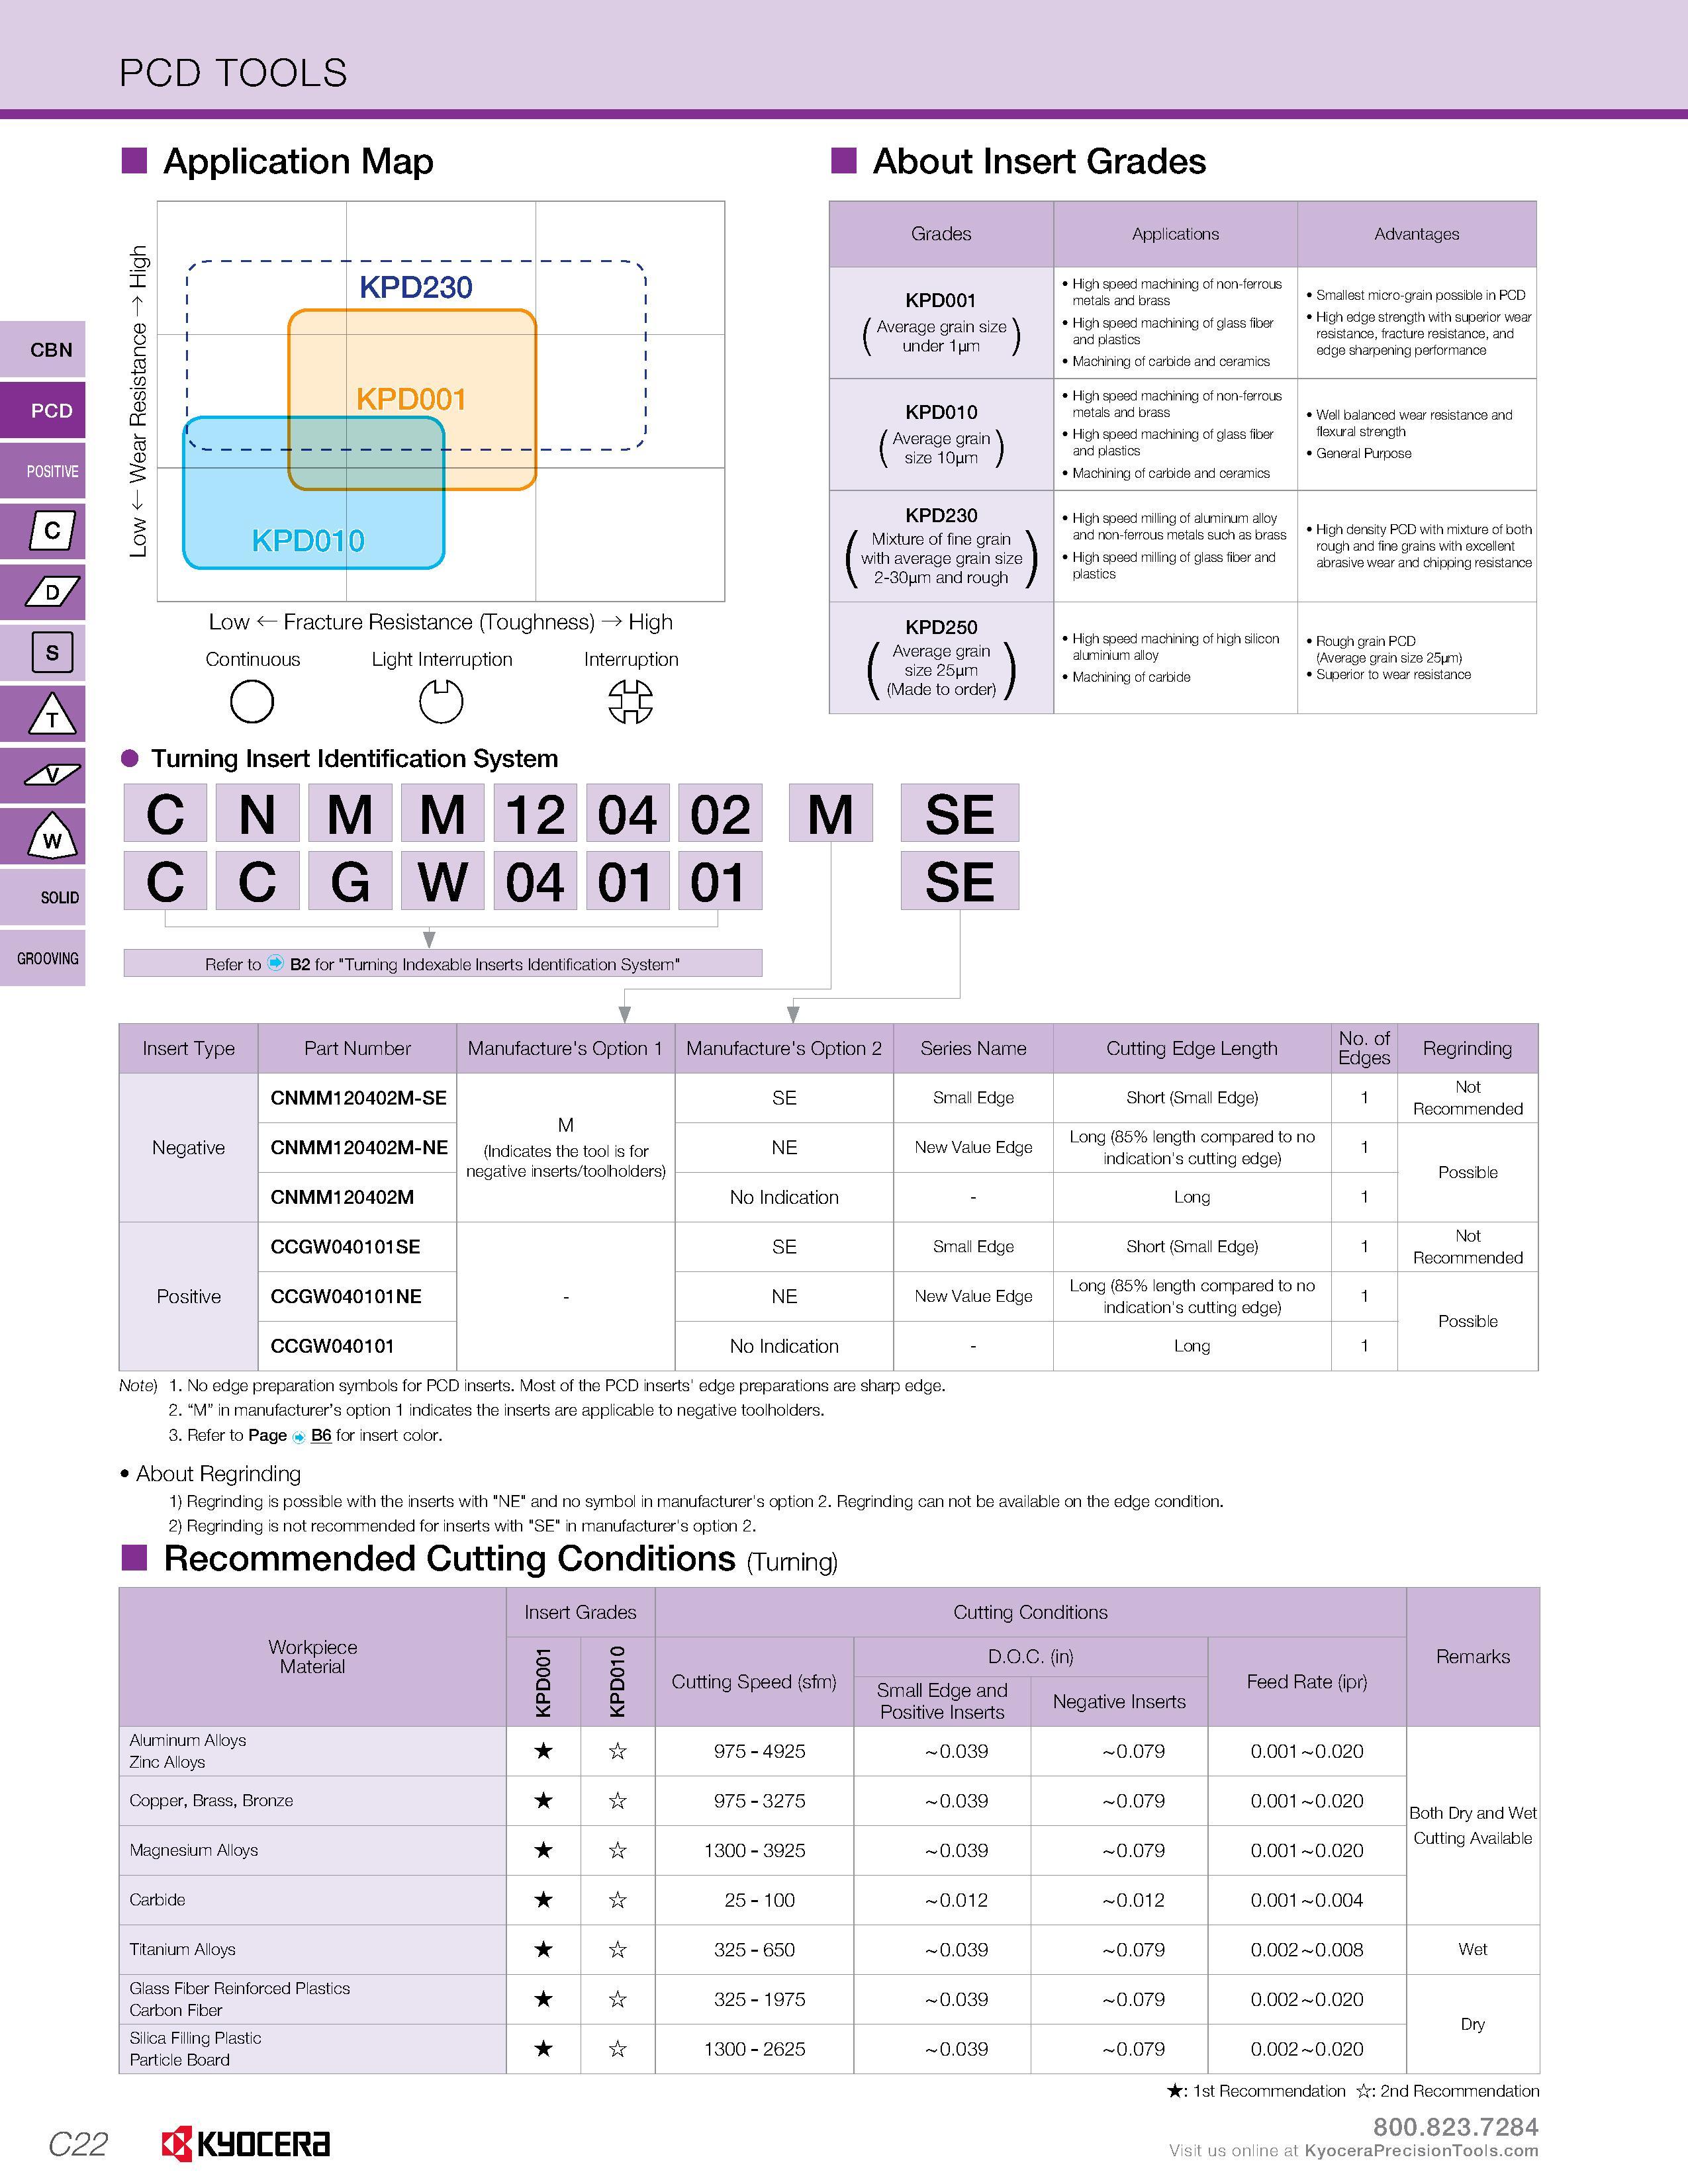
Каталог KYOCERA 2016 Токарные резцы с пластинами Стр. C22 0150 ENG Lab2u PCD TOOLS Application Map About Insert Grades CBN I 0 c % 0 (0 0 5 1 g o KPD01 KPD230 KPD001 -\ Low Fracture Resistance (Toughness) High Continuous Light Interruption Interruption o Turning Insert Identification System C N M M 12 04 02 M SE C C G W 04 01 01 Grades Applications Advantages KPD001 / Average grain size \ \ under 1pm / High speed machining of non-ferrous metals and brass High speed machining of glass fiber and plastics Machining of carbide and ceramics Smallest micro-grain possible in PCD High edge strength with superior wear resistance, fracture resistance, and edge sharpening performance KPD010 / Average grain \ \ size 10pm / High speed machining of non-ferrous metals and brass High speed machining of glass fiber and plastics Machining of carbide and ceramics Well balanced wear resistance and flexural strength General Purpose KPD230 / Mixture of fine grain \ ( with average grain size ) \ 2-30pm and rough / High speed milling of aluminum alloy and non-ferrous metals such as brass High speed milling of glass fiber and plastics High density PCD with mixture of both rough and fine grains with excellent abrasive wear and chipping resistance KPD250 / Average grain \ ( size 25pm ) (Made to order) High speed machining of high silicon aluminium alloy Machining of carbide Rough grain PCD (Average grain size 25pm) Superior to wear resistance SE Refer to B2 for "Turning Indexable Inserts Identification System" I Insert Type Part Number Manufacture's Option 1 Manufacture's Option 2 Series Name Cutting Edge Length Ndg ° Regrinding Negative CNMM120402M-SE M (Indicates the tool is for negative inserts/toolholders) SE Small Edge Short (Small Edge) Not Recommended CNMM120402M-NE NE New Value Edge Long (85% length compared to no indication's cutting edge) Possible CNMM120402M No Indication Long Positive CCGW040101SE SE Small Edge Short (Small Edge) Not Recommended CCGW040101NE NE New Value Edge Long (85% length compared to no indication's cutting edge) Possible CCGW040101 No Indication Long PCD POSITIVE SOLID GROOVING Note) 1. No edge preparation symbols for PCD inserts. Most of the PCD inserts' edge preparations are sharp edge. 2. “M” in manufacturer’s option 1 indicates the inserts are applicable to negative toolholders. 3. Refer to Page B6 for insert color. About Regrinding 1) Regrinding is possible with the inserts with "NE" and no symbol in manufacturer's option 2. Regrinding can not be available on the edge condition. 2) Regrinding is not recommended for inserts with "SE" in manufacturer's option 2. Recommended Cutting Conditions (Turning) Insert Grades Cutting Conditions Workpiece Material KPD001 KPD010 Cutting Speed (sfm) D.O.C. (in) Small Edge and n ... i . Negative Inserts Positive Inserts a Feed Rate (ipr) Remarks Aluminum Alloys Zinc Alloys 975 - 4925 0.039 0.079 0.001 0.020 Both Dry and Wet Cutting Available Copper, Brass, Bronze 975 - 3275 0.039 0.079 0.001 0.020 Magnesium Alloys 1300 - 3925 0.039 0.079 0.001 0.020 Carbide 25-100 0.012 0.012 0.001 0.004 Titanium Alloys 325 - 650 0.039 0.079 0.002 0.008 Wet Glass Fiber Reinforced Plastics Carbon Fiber 325 - 1975 0.039 0.079 0.002 0.020 Dry Silica Filling Plastic Particle Board 1300-2625 0.039 0.079 0.002 0.020 : 1st Recommendation : 2nd Recommendation C22 Kyocera |
|||||
См.также / See also : |
|||||
Расчет режимов резания при токарной обработке / Turning formulas |
Расчет режимов резания при сверлении / Formulas for drilling |
||||
Аналоги сталей Таблицы / Workpiece material conversion table |
Расчет режимов резания при фрезеровании / Milling formulas |
||||
Группы конструкционных материалов / Workpiece material groups |
Удельная сила резания / Specific cutting force |
||||
Техника безопасности при работе с инструментом / Metal cutting safety |
Производительность режущего инструмента / Machining economy |
||||
| |
|||||
| KYOCERA | |||||
| |
|||||
 Каталог KYOCERA 2017 Инструмент режущий для металлорежущих станков (англ.яз / ENG) (1072 страницы) |
|||||
 Каталог KYOCERA 2016 Режущий инструмент для станков (англ.яз / ENG) (992 страницы) |
 Каталог KYOCERA 2016 Металлорежущий инструмент для точения на станках (англ.яз / ENG) (679 страниц) |
 Каталог KYOCERA 2016 Фрезерный металлорежущий инструмент с СРП (англ.яз / ENG) (335 страниц) |
 Каталог KYOCERA 2016 Твердосплавный вращающийся режущий инструмент (англ.яз / ENG) (315 страниц) |
 Каталог KYOCERA 2015 Инструмент режущий для мелкоразмерной обработки (англ.яз / ENG) (406 страниц) |
 Каталог KYOCERA 2014 Металлорежущий инструмент (англ.яз / ENG) (885 страниц) |
 Каталог KYOCERA 2011 Металлорежущий инструмент (англ.яз / ENG) (835 страниц) |
|||||
| |
|||||
|
Каталоги инструмента и оснастки для металлообработки на станках / Cutting tools and tooling system catalogs |
|||||
| Каталог KYOCERA 2016 Металлорежущий инструмент для точения на станках (Всего 679 стр.) | |||||
| |
|||||
 147 |  148 |  149 |  151 |  152 |  153 |
|
Lab2U | Catalogs | Tap drill sizes | Speed to RPM | Material table Разработчики сайта / Developers of site |
|
Поиск на сайте Lab2u.ru с помощью поисковых систем ЯНДЕКС, BING, GOOGLE:
|
||
|
|
||
