| Обновлено 2020-04-16 13:10:01 |
|
Режущий инструмент, инструментальная оснастка и приспособления / Cutting tools, tooling system and workholding
WALTER | Каталог WALTER 2012 Инструмент и оснастка Valenite (Всего 2590 стр.) |
|||||
|
862 Каталог WALTER 2012 Металлорежущий инструмент и инструментальная оснастка Valenite Стр.B364 |
|||||
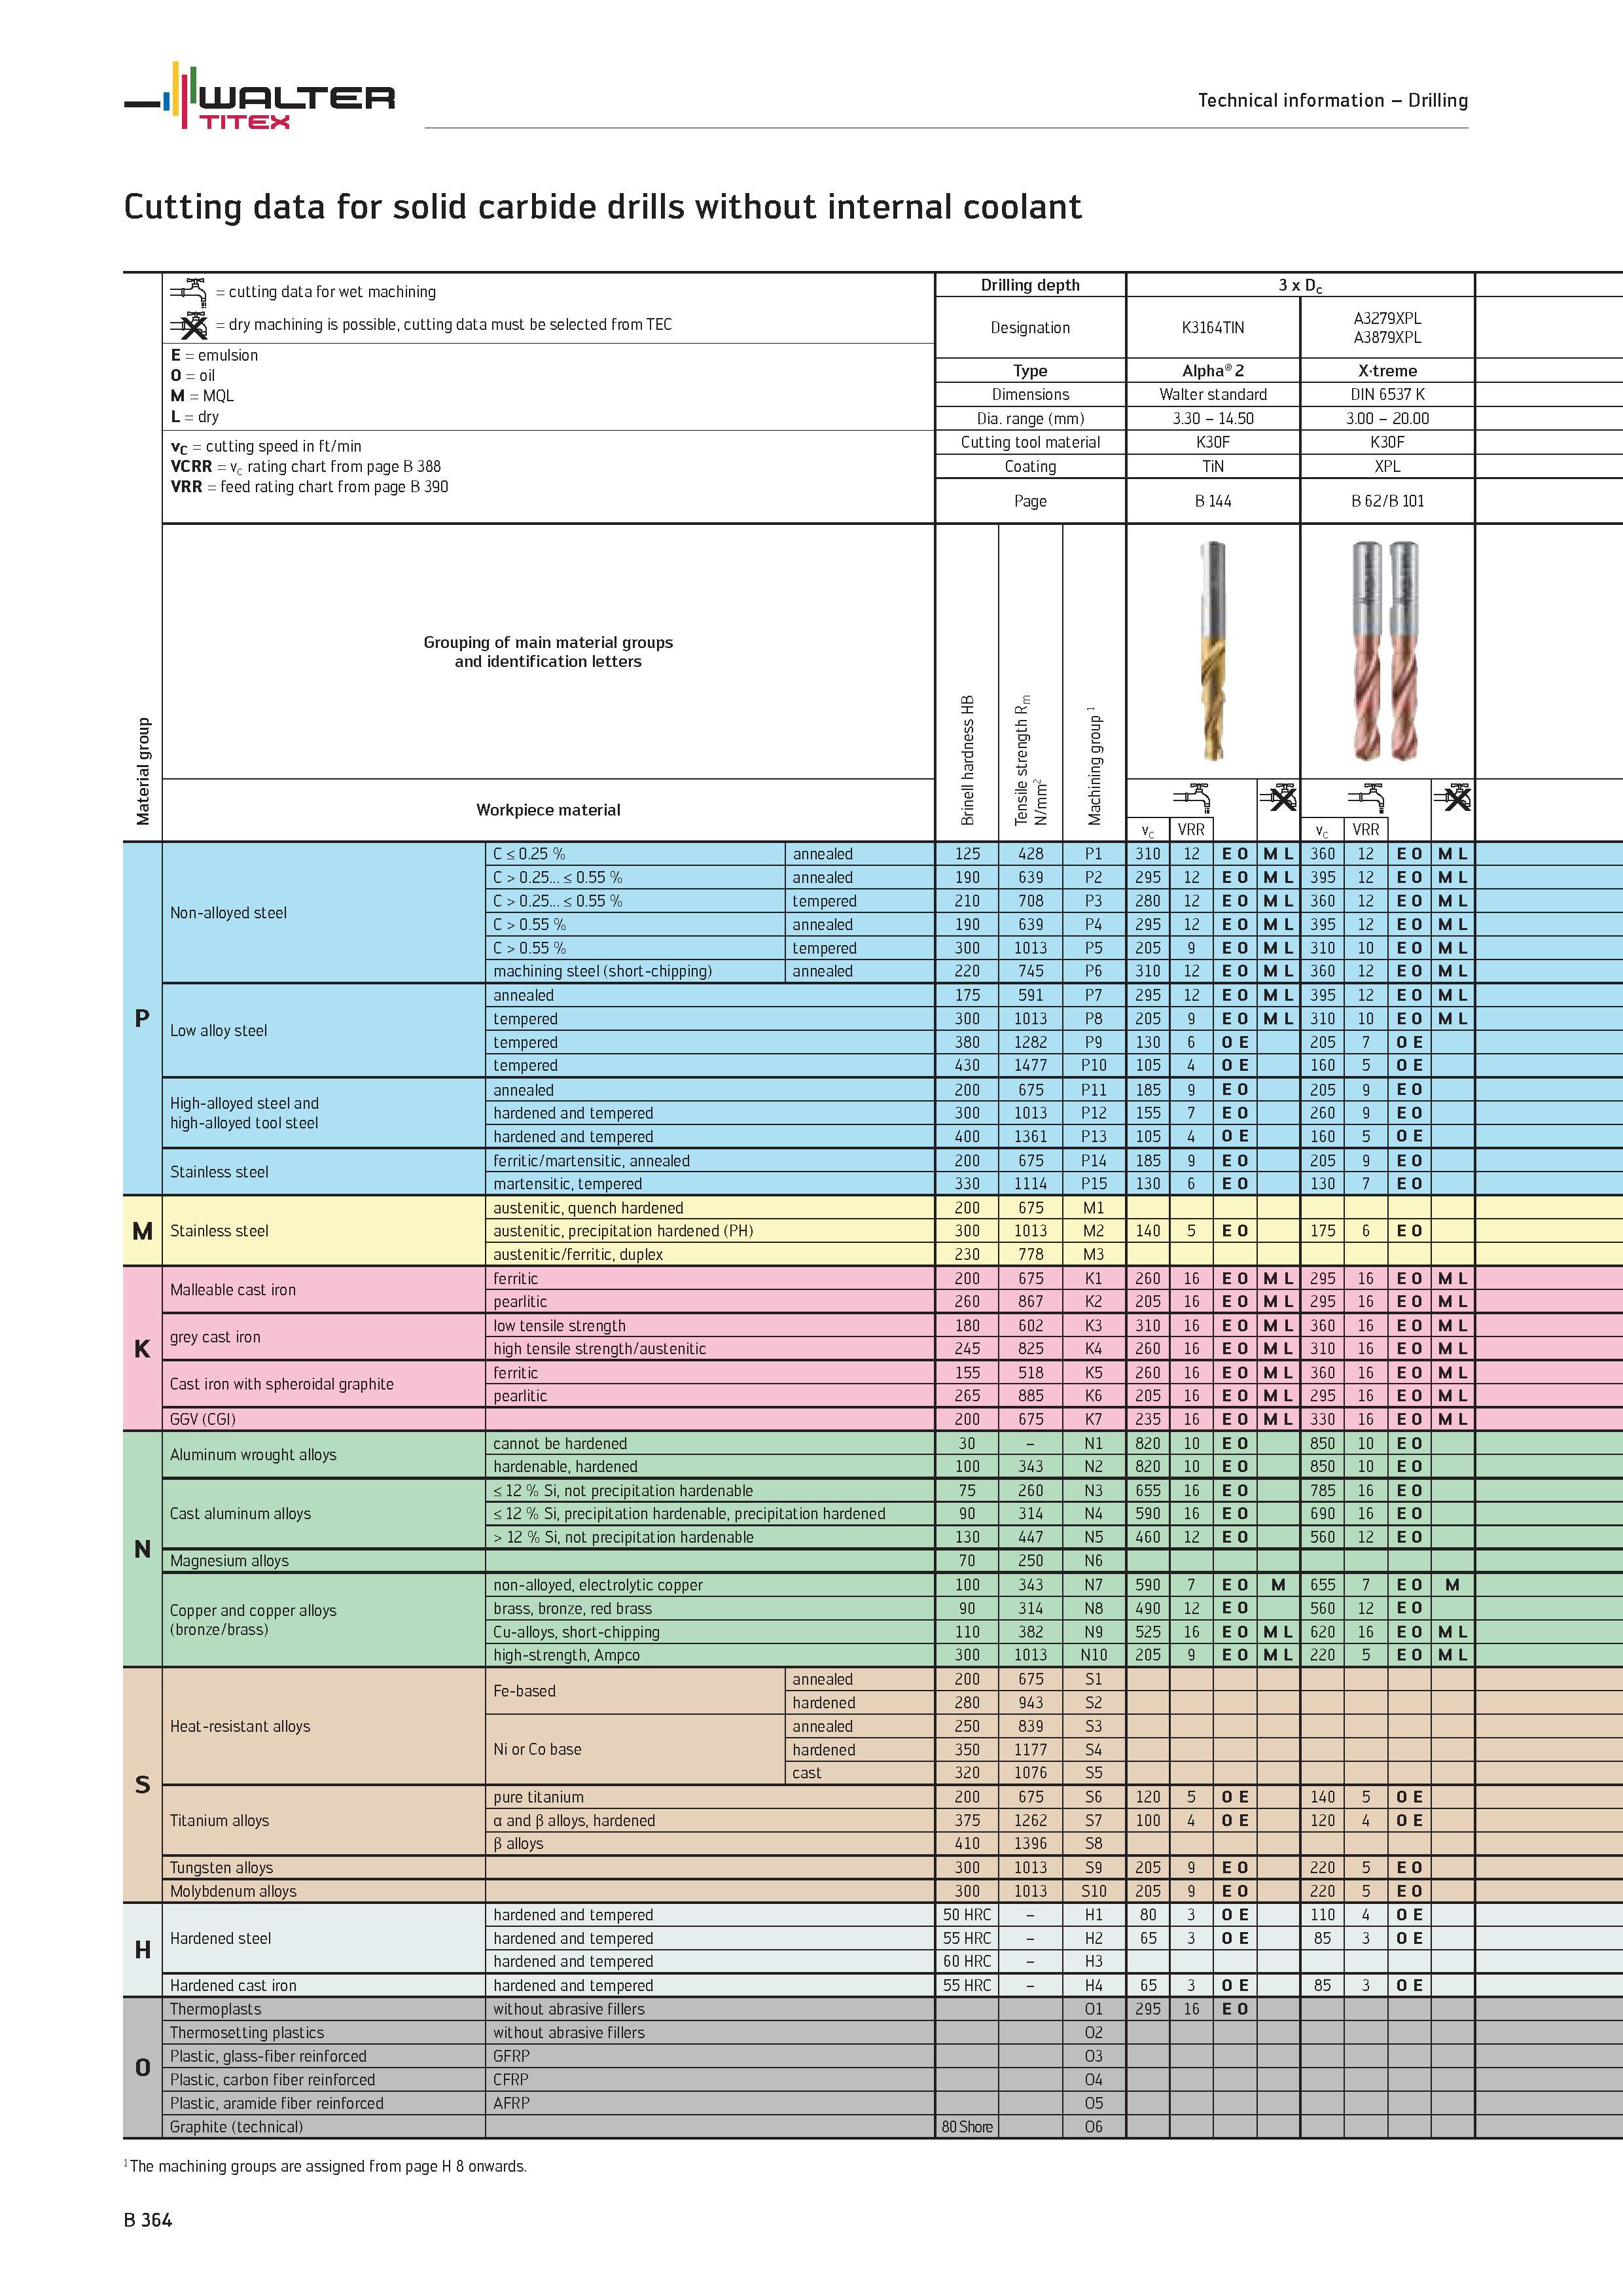
Cutting data for solid carbide drills WALTER TITEX without internal coolant Material group cutting data for wet machining dry machining is possibCutting data for solid carbide drills WALTER TITEX without internal coolant Material group cutting data for wet machining dry machining is possible, cutting data must be selected from TEC Drilling depth 3 x Dc Designation K3164TIN A3279XPL A3879XPL E emulsion O oil M MQL L dry Type Alpha 2 Xtreme Dimensions Walter standard DIN 6537 K Dia. range (mm) 3.30 14.50 3.00 20.00 vc cutting speed in ft/min VCRR vc rating chart from page B 388 VRR feed rating chart from page B 390 Cutting tool material K30F Coating TiN XPL Page B 144 B62/B 101 Grouping of main material groups and identification letters Brinell hardness HB Tensile strength Rm N/mm2 Machining group 1 Workpiece material 3 3 Vc VRR Vc VRR p Non-alloyed steel C < 0.25 % annealed 125 428 P1 310 12 360 12 C > 0.25 < 0.55 % annealed 190 639 P2 295 12 395 12 C > 0.25 < 0.55 % tempered 210 708 P3 280 12 360 12 C > 0.55 % annealed 190 639 P4 295 12 395 12 C > 0.55 % tempered 300 1013 P5 205 310 10 machining steel (short-chipping) annealed 220 745 P6 310 12 360 12 Low alloy steel annealed 175 591 P7 295 12 395 12 tempered 300 1013 P8 205 310 10 tempered 380 1282 P9 130 O E 205 O E tempered 430 1477 P10 105 4 O E 160 5 O E High-alloyed steel and high-alloyed tool steel annealed 200 675 P11 185 205 hardened and tempered 300 1013 P12 155 260 hardened and tempered 400 1361 P13 105 4 O E 160 5 O E Stainless steel ferritic/martensitic, annealed 200 675 P14 185 205 martensitic, tempered 330 1114 P15 130 130 M Stainless steel austenitic, quench hardened 200 675 M1 austenitic, precipitation hardened (PH) 300 1013 M2 140 5 175 austenitic/ferritic, duplex 230 778 M3 K Malleable cast iron ferritic 200 675 K1 260 16 295 16 pearlitic 260 867 K2 205 16 295 16 grey cast iron low tensile strength 180 602 K3 310 16 360 16 high tensile strength/austenitic 245 825 K4 260 16 310 16 Cast iron with spheroidal graphite ferritic 155 518 K5 260 16 360 16 pearlitic 265 885 K6 205 16 295 16 GGV (CGI) 200 675 K7 235 16 330 16 N Aluminum wrought alloys cannot be hardened 30 N1 820 10 850 10 hardenable, hardened 100 343 N2 820 10 850 10 Cast aluminum alloys < 12 % Si, not precipitation hardenable 75 260 N3 655 16 785 16 < 12 % Si, precipitation hardenable, precipitation hardened 90 314 N4 590 16 690 16 > 12 % Si, not precipitation hardenable 130 447 N5 460 12 560 12 Magnesium alloys 70 250 N6 Copper and copper alloys (bronze/brass) non-alloyed, electrolytic copper 100 343 N7 590 M 655 M brass, bronze, red brass 90 4 31 N8 490 12 560 12 Cu-alloys, short-chipping 110 382 N9 525 16 620 16 high-strength, Ampco 300 1013 N10 205 220 5 S Heat-resistant alloys Fe-based annealed 200 675 S1 hardened 280 943 S2 Ni or Co base annealed 250 839 S3 hardened 350 1177 S4 cast 320 1076 S5 Titanium alloys pure titanium 200 675 S6 120 5 O E 140 5 O E a and p alloys, hardened 375 1262 S7 100 4 O E 120 4 O E P alloys 410 1396 S8 Tungsten alloys 300 1013 S9 205 220 5 Molybdenum alloys 300 1013 S10 205 220 5 H Hardened steel hardened and tempered 50 HRC H1 80 3 O E 110 4 O E hardened and tempered 55 HRC H2 65 3 O E 85 3 O E hardened and tempered 60 HRC H3 Hardened cast iron hardened and tempered 55 HRC H4 65 3 O E 85 3 O Thermoplasts without abrasive fillers O1 295 16 Thermosetting plastics without abrasive fillers O2 Plastic, glass-fiber reinforced GFRP O3 Plastic, carbon fiber reinforced CFRP O4 Plastic, aramide fiber reinforced AFRP O5 Graphite (technical) 80 Shore O6 1 The machining groups are assigned from page H 8 onwards. B 364 Technical information Drilling |
|||||
См.также / See also : |
|||||
Металлообработка Учебники и справочники / Metal Cutting Technology Technical Guide |
Особенности сверления металла / Drill a hole in metal |
||||
Токарная обработка металла / Basics of metal turning |
Фрезерование на фрезерном станке / Basics of milling |
||||
Нарезание резьбы метчиками / Tapping |
Развертывание отверстий и развертки по металлу / Reaming and reamer cutting tool |
||||
Расточка на токарном станке / Boring on a lathe |
Растачивание отверстий на расточном станке / Boring on a boring machine |
||||
| |
|||||
| WALTER | |||||
| |
 Каталог WALTER 2017 Инструмент и оснастка для станков (2605 страниц) |
 Каталог WALTER 2016 Общий Инструмент режущий и оснастка (нем.яз. / DEU) (2605 страниц) |
 Каталог WALTER 2016 Новый инструмент для металлообработки Вер. 16-2 (276 страниц) |
 Каталог WALTER 2016 Продукция для металлообработки Инновации Вер. 16-1 (116 страниц) |
 Каталог WALTER 2015 Новый инструмент и оснастка 2015-1 (336 страниц) |
 Каталог WALTER 2014 Новая продукция 14-2 (324 страницы) |
 Каталог WALTER 2013 Новая инструментальная продукция Инновации Вер 13-1 (276 страниц) |
 Каталог WALTER 2013 Дополнение к общему (832 страниц) |
 Каталог WALTER 2012 Новинки Инструмент для мехобработки Вер 12-2 (232 страницы) |
 Каталог WALTER 2012 Инструмент и оснастка (2148 страниц) |
 Каталог WALTER 2012 Инструмент и оснастка Valenite (англ.яз / ENG) (2590 страниц) |
 Каталог WALTER 2008 Новый металлорежущий инструмент (215 страниц) |
 Каталог WALTER 2007 Режущий инструмент и оснастка (830 страниц) |
|||||
| |
|||||
|
Каталоги инструмента и оснастки для металлообработки на станках / Cutting tools and tooling system catalogs |
|||||
| Каталог WALTER 2012 Инструмент и оснастка Valenite (Всего 2590 стр.) | |||||
| |
|||||
 859 |  860 |  861 |  863 |  864 |  865 |
|
Lab2U | Catalogs | Tap drill sizes | Speed to RPM | Material table Разработчики сайта / Developers of site |
|
Поиск на сайте Lab2u.ru с помощью поисковых систем ЯНДЕКС, BING, GOOGLE:
|
||
|
|
||
